This article is prepared by the WAFU B2B Engineering Team for export buyers, system integrators, and OEM/ODM procurement teams. WAFU Smart Lock was founded in 2013 and focuses on B2B smart lock solutions, with ISO 9001:2015 certification, CE/FCC/RoHS global compliance, and customers across 20+ countries and regions in Europe, Russia, Southeast Asia, and beyond. Please credit the source when reprinting.
Key Dimensions at a Glance
01 Technical Compliance
Traceable across design, testing, and production—not a stack of PDFs.
02 Quality Control
Lab-quantified data for reliability and environmental adaptability.
03 Supply Chain Transparency
Traceable critical components, dual-source redundancy, and lead-time risk alerts.
04 Technology Iteration
A written update, spare-parts, version and end-of-life plan that can be checked against the order.
1. Opening: An Export Sourcing Trap Deeper Than You Think
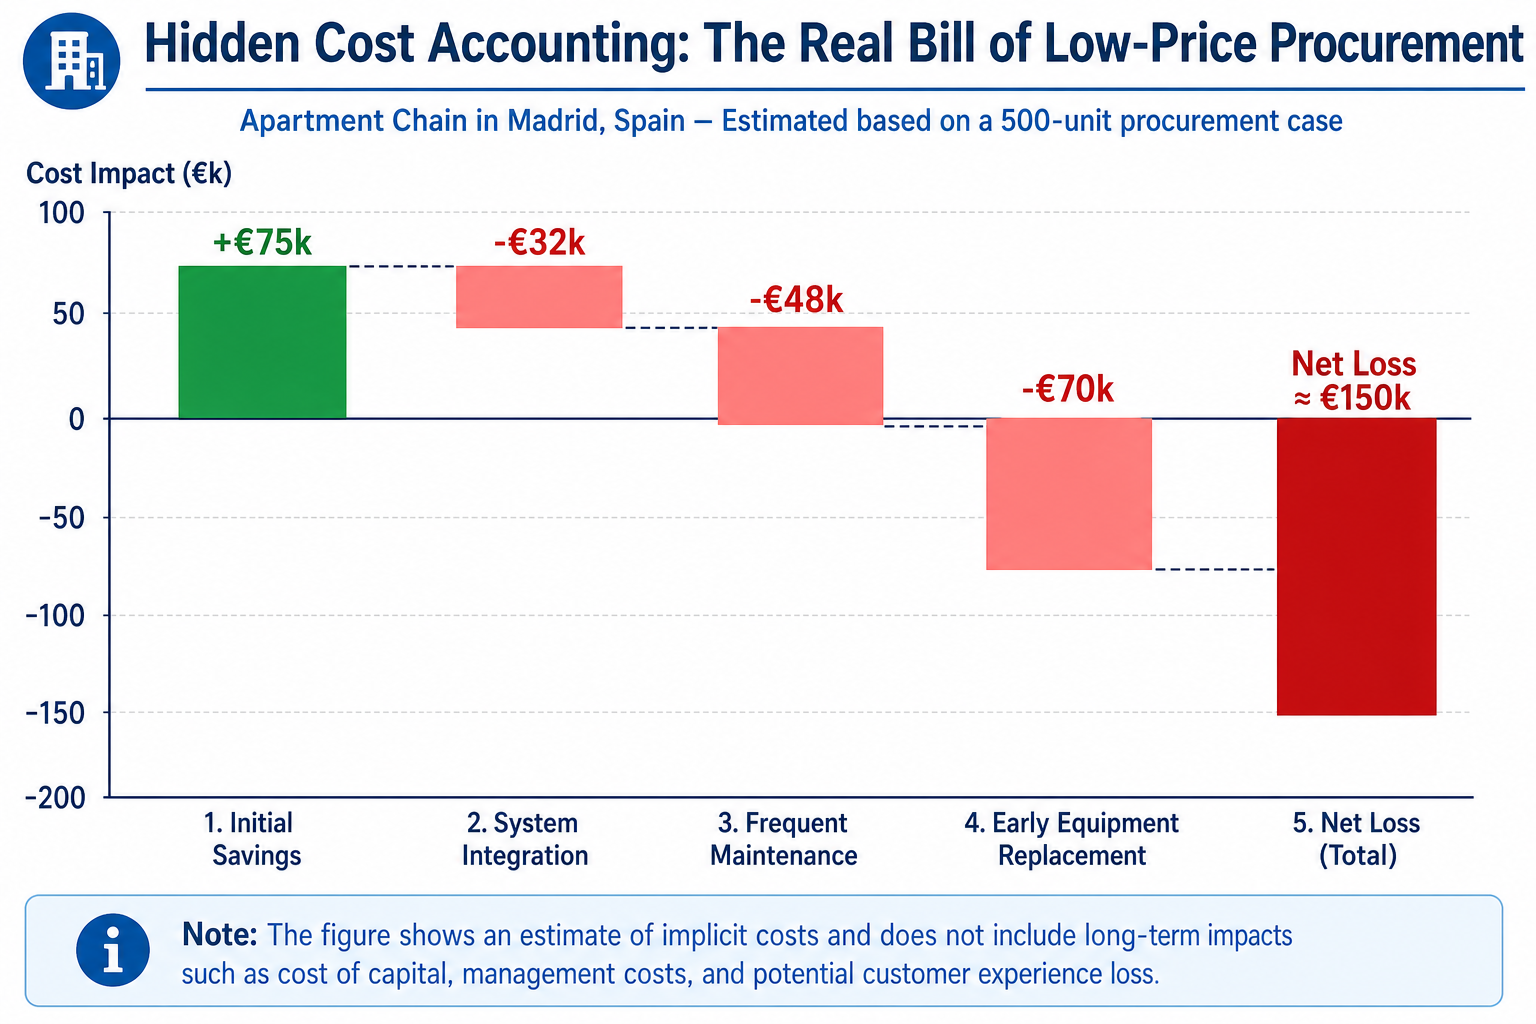
In 2023, a Spanish distributor sourced 500 smart door locks in Shenzhen for a Madrid apartment chain. The purchasing manager chose the lowest bidder—15% below the market average. At signing, the supplier provided a full set of CE and FCC certificates; the datasheet looked perfect.
Six months later, problems surfaced.
After the first 200 locks were installed, the property management system could not sync room status with the locks. The technical team found that the so-called “API” was an ad-hoc HTTP endpoint—neither RESTful nor secured with OAuth 2.0. Temporary PIN codes had to be generated manually in a local admin console and could not link to the front-desk system.
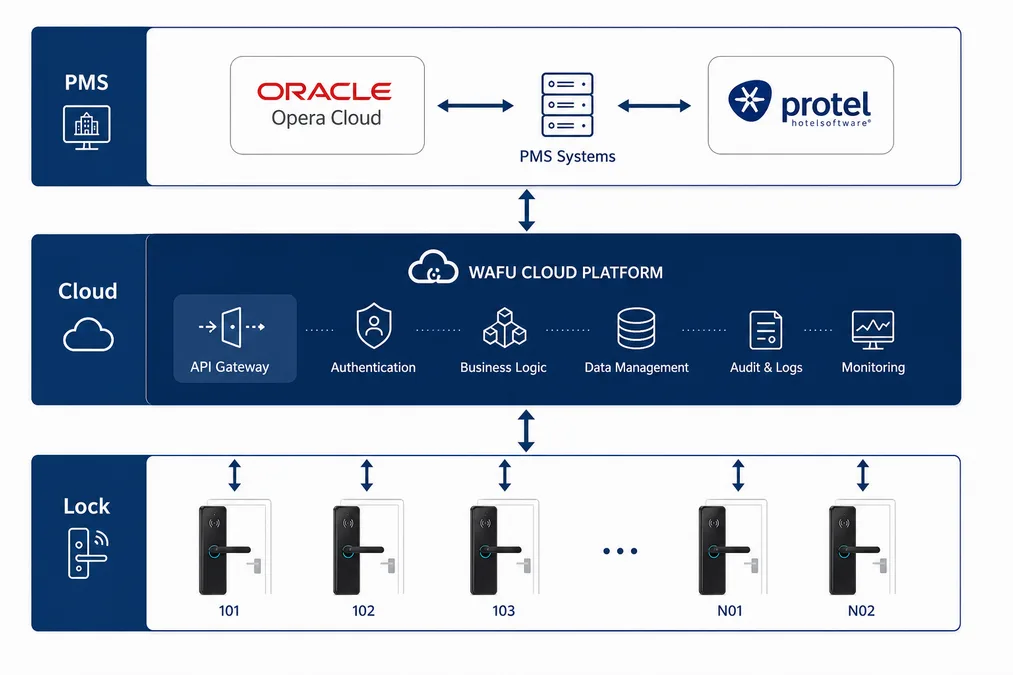
The larger lesson is that a low quotation can hide integration work, replacement parts, version changes and support limits. Treat this scenario as an illustrative risk model, not as a WAFU customer case or a universal failure rate. Ask for the component source, test condition, shipped hardware and firmware version, and written support boundary before comparing prices.
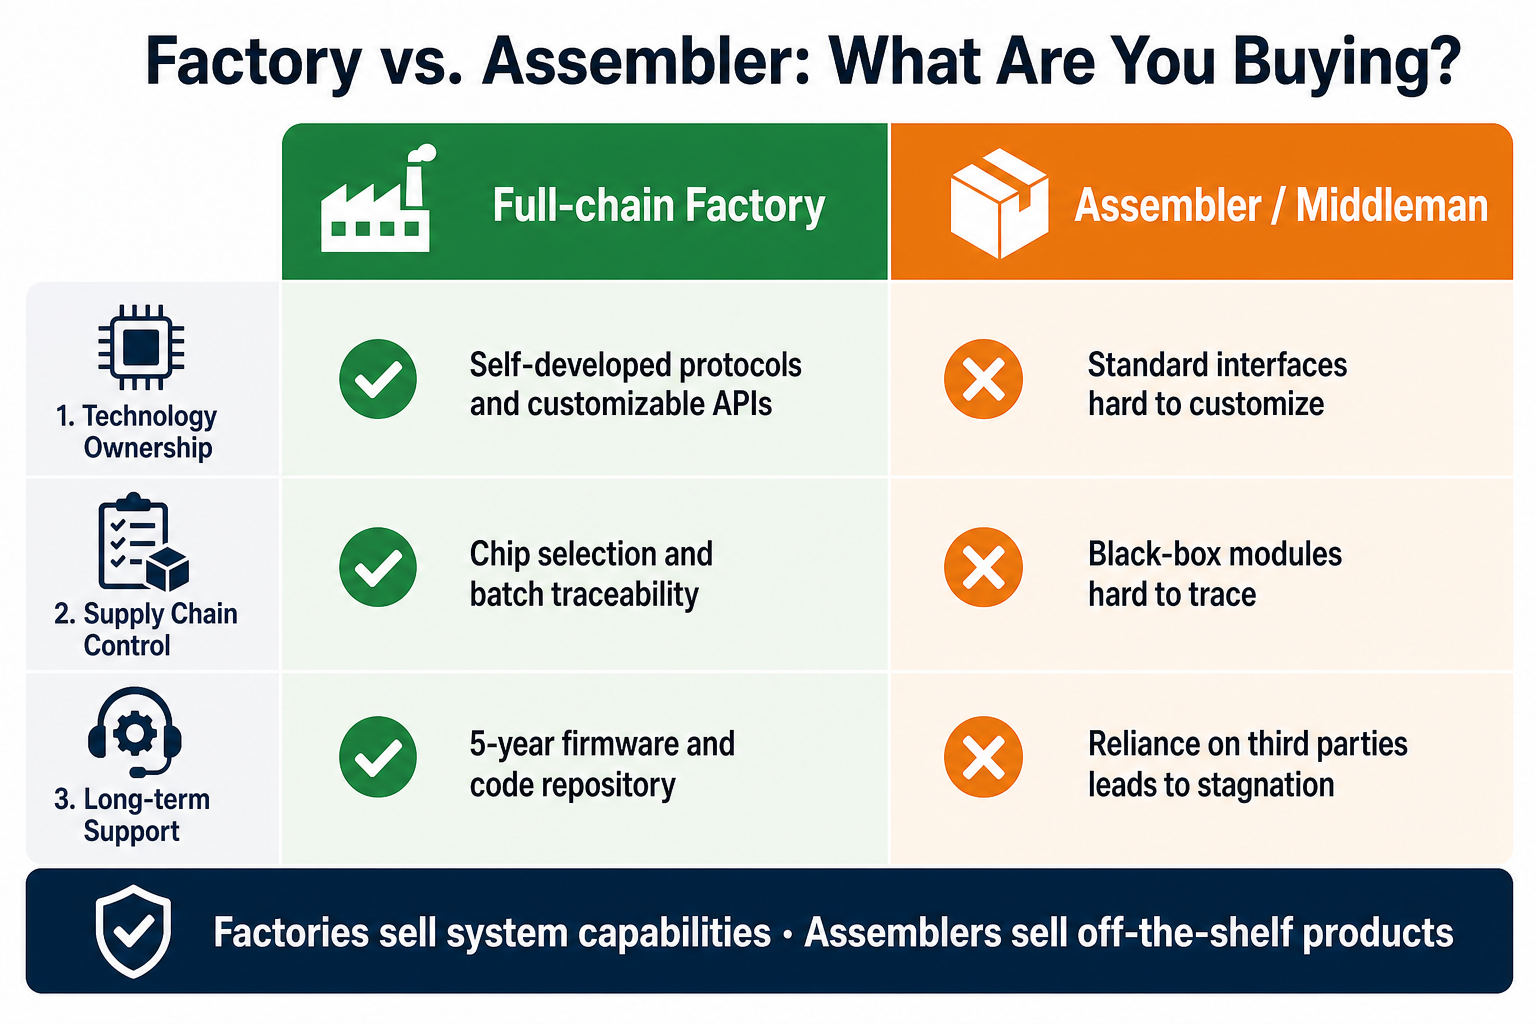
This is not an isolated case. In Shenzhen’s smart lock cluster, price wars have produced two kinds of suppliers: factories and “assemblers.” The former own the full chain from chip selection and PCB design to firmware and certification testing. The latter buy ready-made modules and assemble them—technical depth stops at “it powers on.”
When you only compare FOB price, you are comparing two completely different product lifecycles. One sells a system solution built for 10 years of reliable operation; the other sells hardware that can pass outgoing inspection. That gap in understanding is the first—and deepest—trap in export procurement.
2. Factory vs. Middleman: What Are You Buying?
To see the difference, look past the surface at three dimensions: technology ownership, supply chain control, and long-term support commitment.
Technology Ownership Determines Product Flexibility
Technology ownership should be verified against the exact supplier and configuration. If a supplier presents a branded protocol such as SecureMesh™, ask for the applicable specification, interface documentation, test records and ownership statement before treating it as an integration capability. For PMS work, confirm whether the supplier can adjust packet structures, timing or APIs, and record those boundaries in the quotation or development agreement (see also our OEM/ODM sourcing white paper). Do not assume that a factory or intermediary can customize beyond the documented interface.
Supply Chain Control Determines Quality Consistency
Factories build quality from chip selection. Critical parts such as NXP MCUs and Goodix fingerprint sensors may sit under a 6-month safety-stock policy with multi-source suppliers. Every incoming lot is fully inspected for electrical consistency. Middlemen buy “black-box modules,” cannot trace component lots, and cannot guarantee batch-to-batch performance. When chips go short, factories can qualify alternatives quickly; middlemen wait—as seen in OEM projects for premium residential deployments.
Long-term Support Determines Product Lifecycle
A credible lifecycle plan identifies who owns the firmware, how security fixes are released, which hardware and firmware versions remain supported, and how spare parts or end-of-life changes are communicated. Support should be documented in the quotation, sample approval or agreement rather than treated as an open-ended promise.
The essential difference: factories sell system capability; middlemen sell off-the-shelf goods.
When you buy smart locks, you are also buying a support and change-control process. A supplier should show how that process applies to the exact model and configuration being sampled.
3. Four Core Dimensions for a Factory Audit
Dimension 1: Technical Compliance Is a System, Not a Stack of PDFs
Most suppliers’ “certificates” are result documents only. Real technical compliance means folding regulatory requirements into product specs at design time, covering them fully in testing, and executing them with traceability in production.
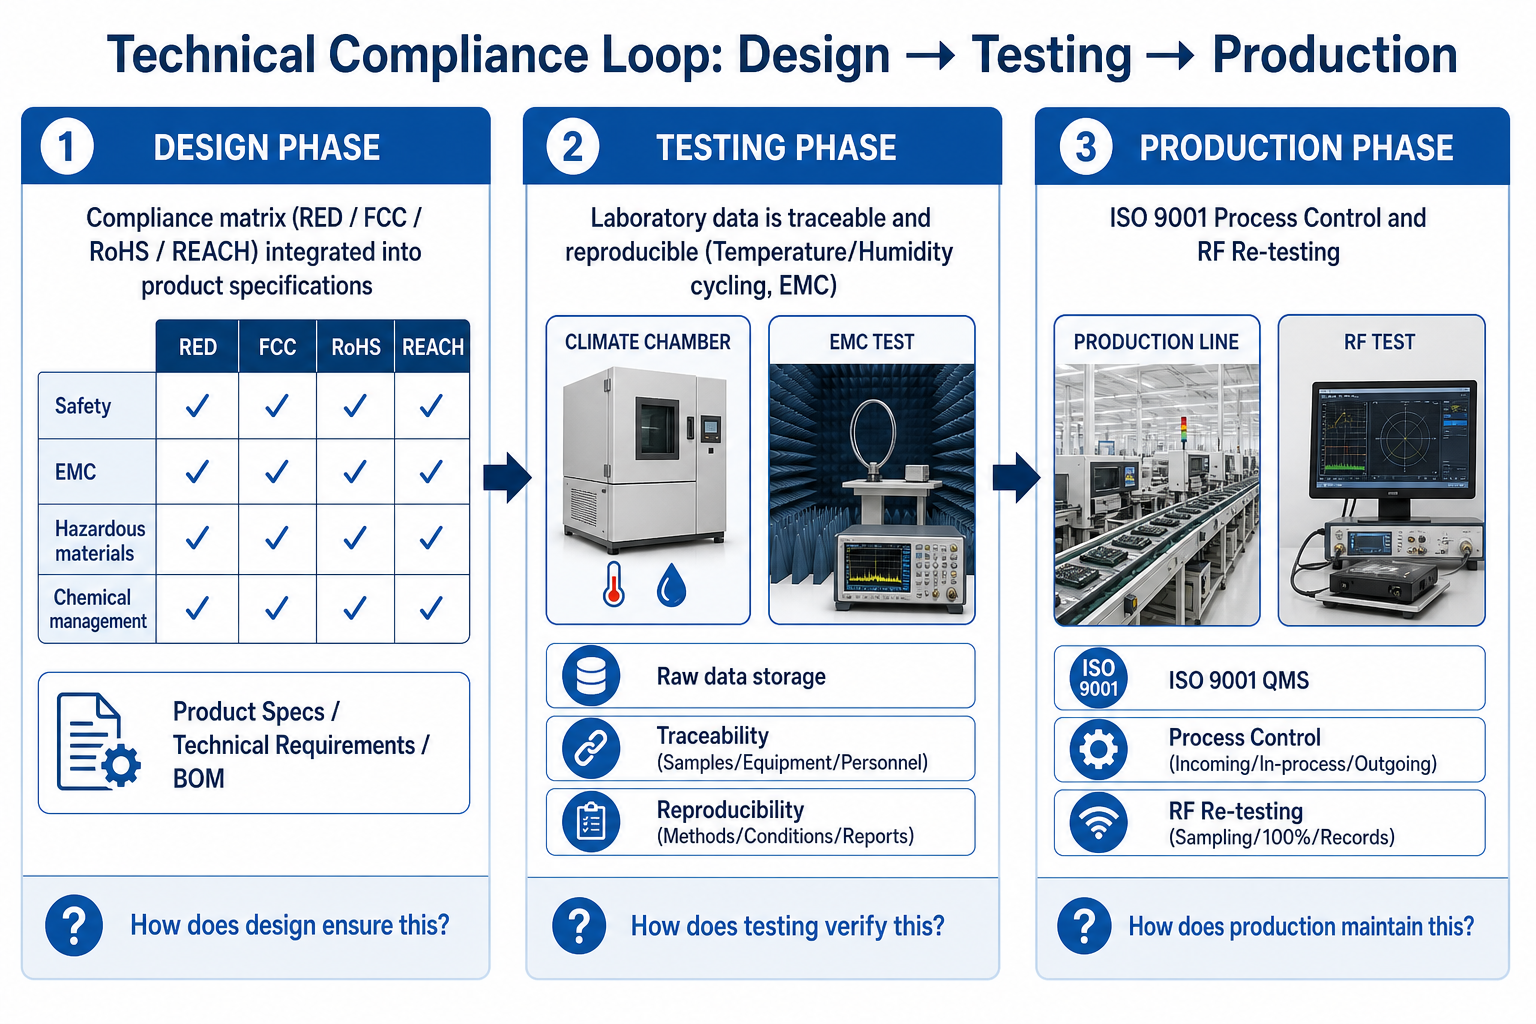
Design stage: compliance as a design constraint
At a capable factory, the design team builds a compliance matrix at product definition. Applicable requirements such as EU RED, FCC Part 15, RoHS and REACH become concrete design and test items, mapped to the exact radio module, hardware revision and intended market.
Testing stage: lab data behind compliance claims
Internal labs run intensified tests based on IEC 60068, EN 14846, and related standards—about 20% stricter than typical industry practice (comparative analysis against those standards). Environmental tests cover −40°C to 85°C temperature/humidity cycling; EMC includes radiated emissions, immunity, ESD, and the full suite. Each report maps to a specific hardware version, firmware version, and test condition—traceable and reproducible. Middlemen often provide “generic model” reports that differ from shipped product versions.
Production stage: process control for consistency
ISO 9001 embeds compliance into production. Critical steps such as RF module soldering and antenna matching have control points; each lot is sampled for RF re-test. Compliance is not “sample pass”—it is “process assurance.”
A real compliance system answers three questions: (1) How does design ensure compliance? (2) How does testing verify it? (3) How does production maintain it? If a supplier can only hand over PDFs and cannot explain these three points, “compliance” may be paperwork only.
Dimension 2: Quality Control Is Lab Data, Not Just a Production Line
On a factory tour, automation on the line is easy to notice. Real quality decisions come from quantified laboratory data.
Reliability data drives maintenance cost
Request a mechanical life report, motor test method, sample size, acceptance criteria and test-to-shipment link. A cycle count or MTBF estimate is meaningful only when the test conditions, model, configuration and calculation method are disclosed.
Performance data drives user experience
Authentication testing should state the method, user sample, environmental conditions and acceptance criteria. When a supplier says recognition is fast or reliable, ask which model and firmware were tested and whether the result applies to the supplied configuration.
Environmental data drives deployment range
Environmental data should state temperature, humidity, duration, enclosure condition and pass criteria. Indoor test data must not be presented as proof of outdoor or extreme-climate suitability.
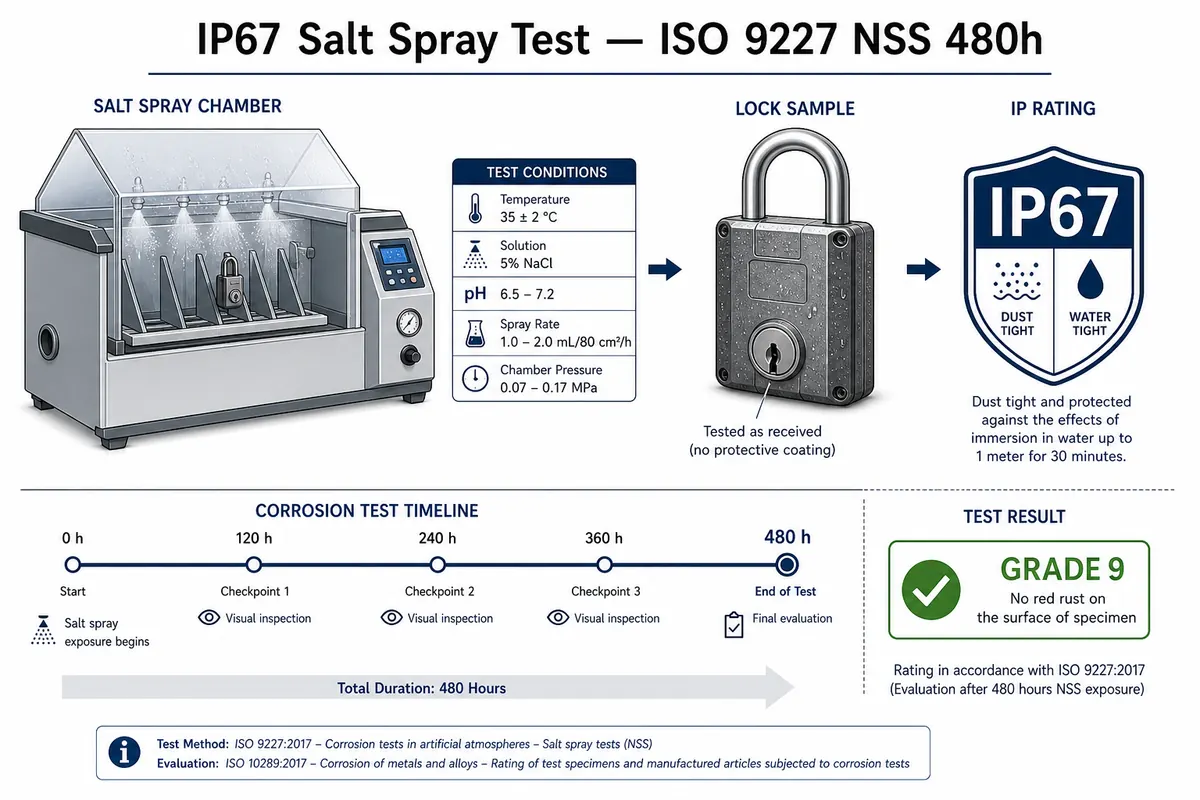
The core value of quality control is turning uncertainty into measurable risk with lab data. When a supplier cannot provide a complete test data package, you are carrying unknown technical risk.
Dimension 3: Supply Chain Transparency Is Risk Control, Not Just a BOM
A BOM tells you what is used. Transparency tells you where components come from, whether supply is stable, and how issues are handled.
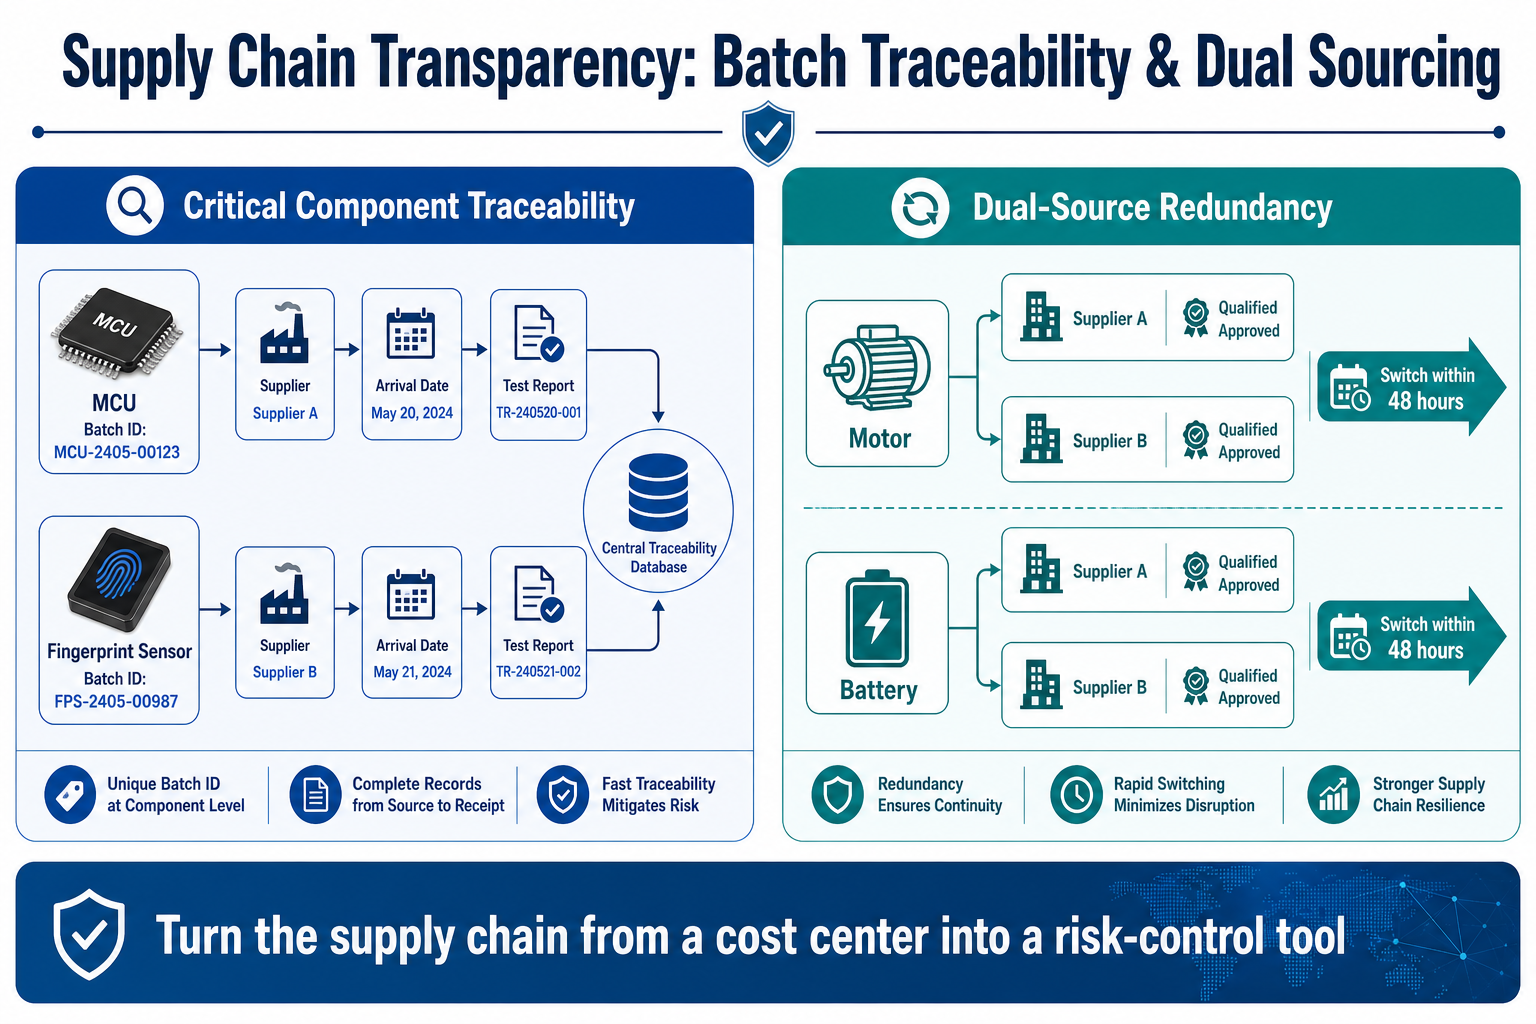
Traceable critical components
Each MCU and fingerprint sensor carries a unique code linked to supplier, arrival date, and test report. Quality issues can be isolated to affected lots instead of a full line recall.
Supplier redundancy
Motors, batteries, and other critical parts should have qualified alternatives or a documented substitution process. Any replacement must be reviewed for fit, electrical behavior, reliability and certification impact before release.
Risk early-warning
Models based on chip lead times, material prices, and geopolitics trigger alternative evaluation when, for example, a chip’s lead time stretches from 8 to 20 weeks.
Transparency turns the supply chain from a cost center into a risk-control tool. If a supplier cannot explain sources, backups, and response mechanisms for critical parts, you carry shortage, quality swing, and delay risk.
Dimension 4: Lifecycle Support Is More Than an OTA Statement
OTA is a feature. Technology iteration is architecture evolution capability.
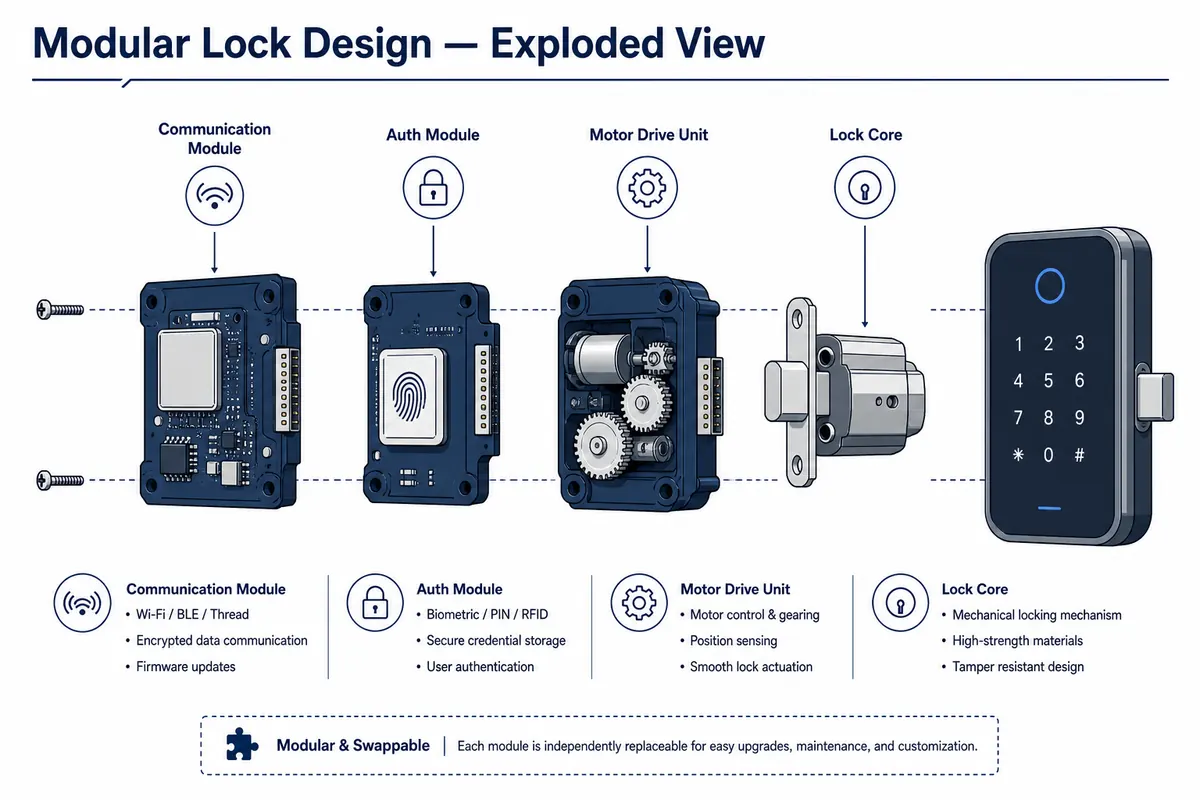
Firmware iteration: continuous feature growth
Modular firmware may support new authentication methods, algorithm improvements or security fixes, but the supported scope must be confirmed for the model and hardware revision.
Hardware iteration: forward-compatible interfaces
Modular designs let the mainboard, communication module, and power management upgrade independently. Supporting a new wireless standard (e.g., Matter) may require only a communication module swap—protecting customer investment.
Ecosystem iteration: standards follow-through
Active participation in industry standards keeps the architecture ready for the next generation—e.g., Bluetooth 4.2 to 5.3 via firmware update.
A lifecycle commitment should identify the support period, update ownership, compatible hardware revisions, spare-parts policy and end-of-life notice process. If a supplier only mentions OTA without written scope, the buyer still carries lifecycle risk.
4. On-Site Audit: How to See Through the Showroom
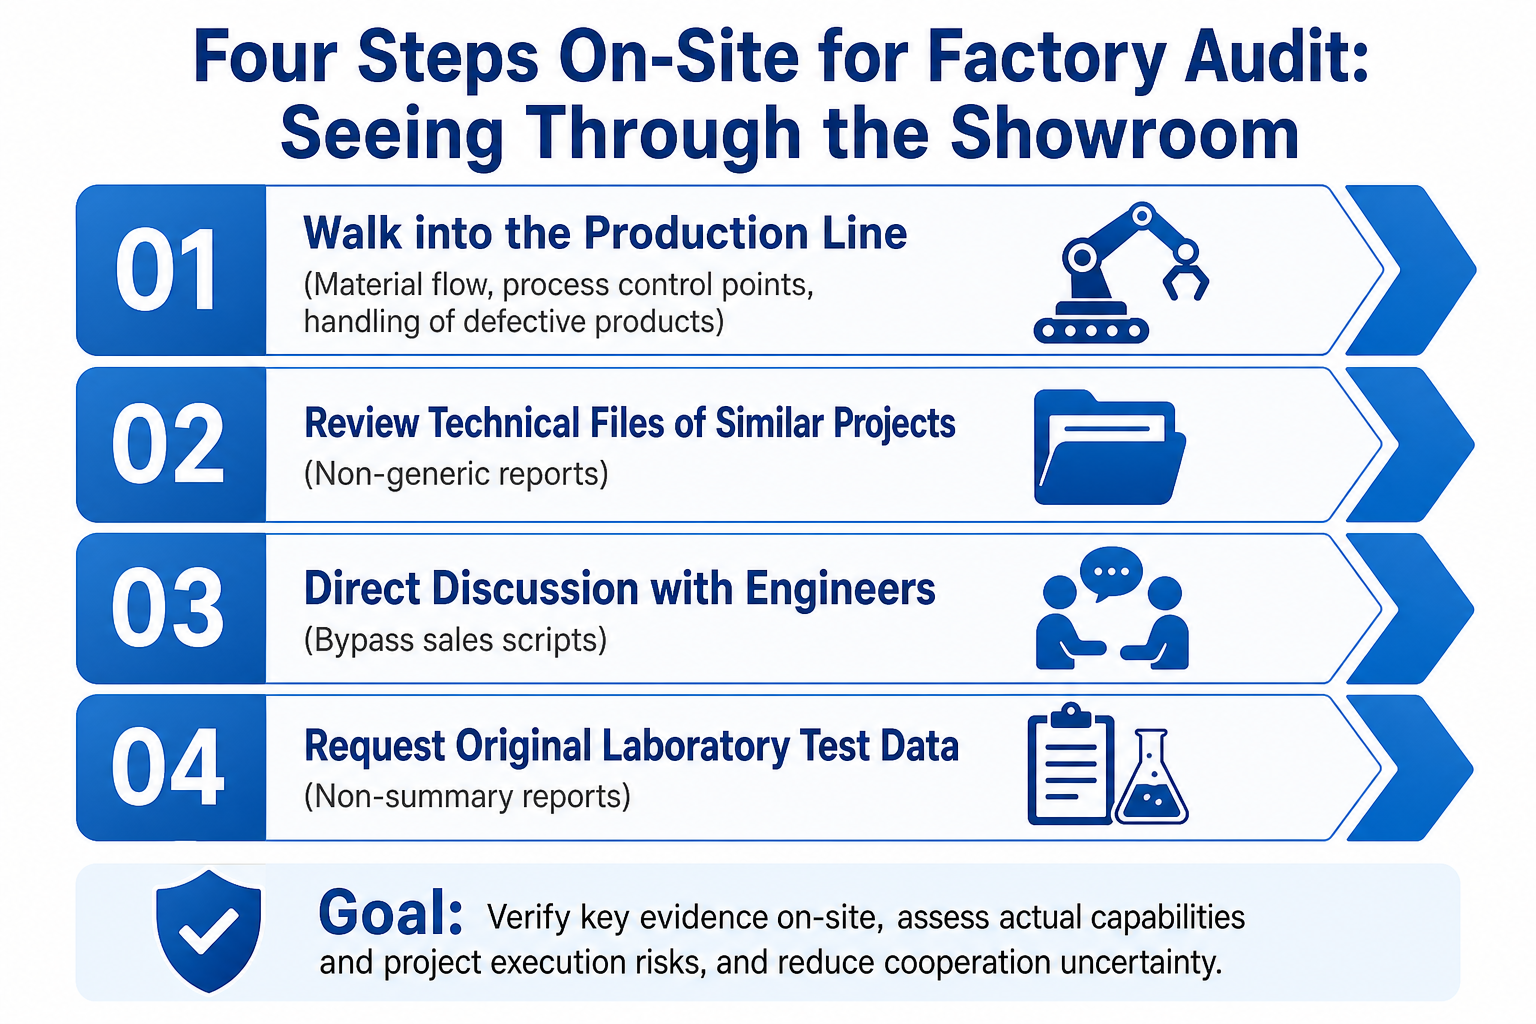
- Skip the staged demo area; walk the production line and observe material flow, process control points, and defective-product handling.
- Do not settle for generic technical reports; request technical files from projects similar to yours.
- Do not stop at sales; discuss concrete technical challenges and solutions with engineers.
- Do not accept verbal promises; insist on original laboratory test data, not summary reports only.
5. Conclusion: Your Procurement Decision Is About More Than Price
All four dimensions point to one core—certainty from technical capability: certain specs, certain costs, certain lifecycle.
Choose a factory and you gain technical control and room to evolve. Choose a middleman and you buy a standardized commodity plus a supply chain that can break at any time.
The former builds long-term advantage: stable systems, controllable cost, autonomous iteration.
The latter plants long-term risk: hard integration, expensive maintenance, technical stagnation.
In this technology-intensive category, the lowest quote is often the most expensive cost. Every cent saved on price can be repaid many times over in repairs, integration, and downtime. Real value is the certainty of full-chain capability—something a price tag cannot measure.
Figures in this article are based on laboratory tests and industry case estimates; actual product performance is subject to project testing.
6. Action Guide: From Evaluation to Decision
Evaluating a smart lock supplier means evaluating whether its technical system can support your project lifecycle.
Prefer suppliers with an owned technology stack and a complete test system.
Act now:
- Review WF-019 invisible lock specifications in the product library
- Book a technical consultation to discuss your project requirements
True cost savings come from long-term stable operation enabled by technical capability.
Continue with OEM/ODM full-process quality control, the invisible lock supply chain guide, and the OEM/ODM sourcing white paper to close the supplier evaluation loop.